Cartoning Machine Selection: Matching the Carton to the Line
The carton is the last thing your customer sees and the first thing that gets value-engineered. It is also sized by the pack inside it, which makes specifying it after the primary machine an expensive habit.

The carton is the last thing your customer sees before they buy, and the first thing that gets "value-engineered" when a project runs over budget.
It is also sized entirely by what goes inside it. Specify the primary pack, then the carton, then the cartoner, and the project is straightforward. Do it in a different order and you get a machine that has to be re-tooled before it runs a single case.
Four ways product gets into a carton
End-load
The carton is erected, product is pushed in horizontally through the open end, and the flaps close. Fast, well proven and the default for wrapped bars, tubes and anything that arrives as a tidy collated group. It suits product that slides cleanly, and a sticky or irregular pack points toward top-load instead.
Top-load
The carton is erected and product is placed in from above. Gentler and far more flexible about arrangement, which makes it the choice for fragile product, mixed contents or any presentation the marketing team cares about. It usually brings pick-and-place equipment with it, and that is what buys the flexibility.
Wrap-around
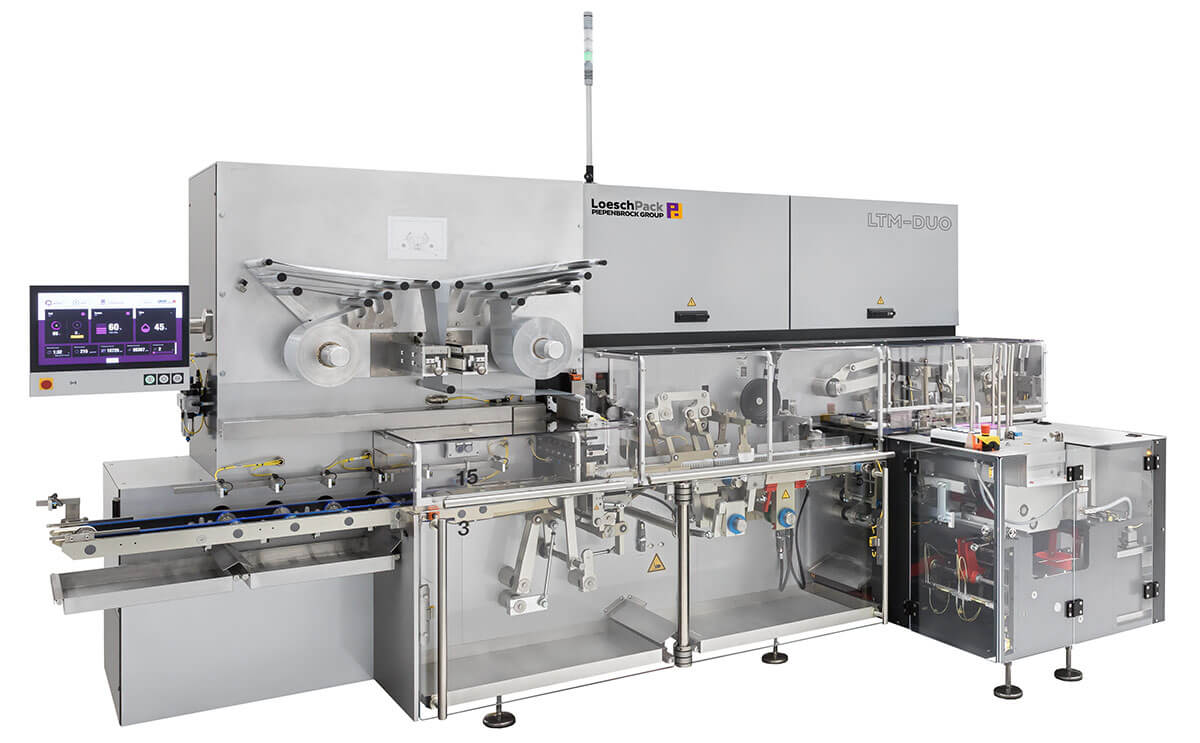
Product is collated first and a flat blank is folded around it. No box is erected and then filled, so there is no wasted volume and the pack is tight to the product. Flat blanks are cheaper than pre-glued cartons, which matters at volume. LoeschPack's CMC uses this approach and runs at speeds of up to 60 cartons per minute.
Display and shelf-ready
A carton built to reach the shelf intact and open into a merchandising unit. Retailers push hard for these because they cut shelf-filling labor, and they are the most demanding format to produce: the pack has to survive transit, tear cleanly along a defined line and still present well once opened.
Counting cartons per minute correctly
Three things, and only one of them is the machine.
- How many primary packs go in each carton. A carton holding a dozen wrapped bars runs at a twelfth of the wrapper's rate and keeps up perfectly well. Compare rates in finished cases per shift, never machine to machine.
- How the product arrives. Cartoners need product collated, counted and correctly oriented. That collation is the harder engineering, and LoeschPack builds it alongside the cartoner so the two are designed as one system.
- Whether your product accumulates. Some primary packs will not stack or queue reliably, including flow packs, three-side seal pouches and slim packs. The CMC handles these through a dedicated add-on module, and specifying that up front is what keeps it out of a field retrofit.
Format range is the expensive question
Cartoning is where SKU proliferation becomes visible. Every carton size needs tooling, and every tooling set is capital plus a place to store it and a changeover to perform.
Ask three questions before the specification is frozen. How many carton sizes must the line run today? How many are likely within five years? And how long does a change take with your own crew, timed at factory acceptance rather than quoted? Machines built with wide format ranges and quick changeover cost more up front and stop being a constraint later.
The CMC platform is offered in in-line and ninety degree layouts, and in right or left hand configurations, which matters more than it sounds: floor space and the direction your existing line runs are usually the first constraints on a project, and the CMC has a layout for both.
Specify it with the primary machine, not after it
The most common and most expensive cartoning mistake is treating it as a later phase. The carton is sized from the primary pack, the collation is designed around how the primary machine discharges, and the two have to agree on timing and fault handling.
When both come from one manufacturer that interface is designed instead of negotiated. LoeschPack builds cartoning to sit downstream of its own wrappers, along with the tray loading and overwrapping around it. Flow wrapper ROI covers sizing the primary machine, and complete and turnkey lines covers when to buy the whole run of it together.
If the cartoner is going into a line that already exists, the interface is the thing to define first, and Piepenbrock Packaging does that with you. Integrating with an existing line covers what to nail down before anyone quotes.
Send us the carton and what goes in it
LoeschPack builds the cartoning and erecting machines alongside the wrapping, feeding and tray loading equipment that feeds them, so the collation and the cartoner are designed as one system by one manufacturer. It has done this since 1919 and builds to ISO 9001 and ISO 14001. Piepenbrock Packaging is the North American arm of the same family-owned group, in business since 1913.
Send us the primary pack, the carton style and every size the line has to run, the count per carton and whether the carton has to reach the shelf as a display unit. Tell us what feeds it and how much floor space you have. You will get the loading method that fits, what the collation has to do, and a clear picture of what the line will deliver before you commit.